-
-
-
-
-
-
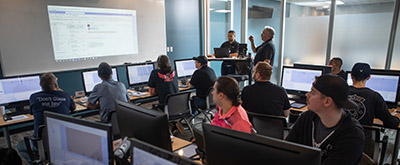
With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.
-
Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
-
-
-
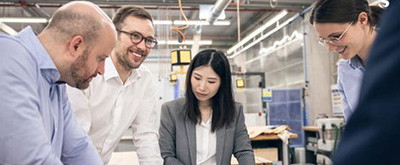
Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.
-
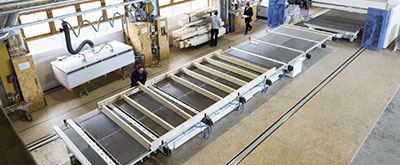
Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.
-
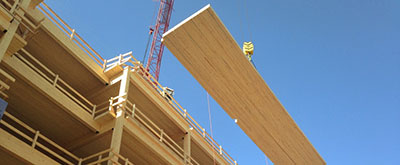
Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.
-
Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
-
-
-
-
-
-
-
With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.
-
Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
-
-
-
Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.
-
Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.
-
Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.
-
Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
-
7 Tips for Choosing a Special Hydraulic Cylinder
Selecting a Special Hydraulic Cylinder is a design decision, not a catalogue exercise. The correct choice affects force, speed, sealing, safety, maintenance, and equipment life. A cylinder may look robust on a test bench yet fail early in a dusty quarry, cold warehouse, or saltwater environment.
Market reports show why careful selection matters. Grand View Research valued the global hydraulic cylinder market at approximately USD 14 billion in 2022 and projected continued growth through 2030. MarketsandMarkets also identifies construction, agriculture, and industrial automation as major demand areas. These forecasts differ in scope and methodology. They are useful signals, not absolute answers. Actual performance still depends on load cycles, fluid cleanliness, mounting accuracy, and operator conditions.
Anthony Esposito, author of Fluid Power with Applications, describes hydraulics as “the science of forces and motions transmitted through liquids.” That principle remains simple. The engineering details are not. This guide presents seven practical tips for choosing a Special Hydraulic Cylinder. It examines bore size, stroke length, pressure rating, rod construction, sealing materials, mounting style, and service support. Look closely at the application. A side-loaded rod, a two-degree alignment error, or contaminated oil can quietly shorten service life. There is no perfect checklist. I have seen specifications appear complete while missing temperature range or retraction speed. That is an uncomfortable lesson. Confirm every critical value with the manufacturer, relevant ISO standards, and field data before ordering.
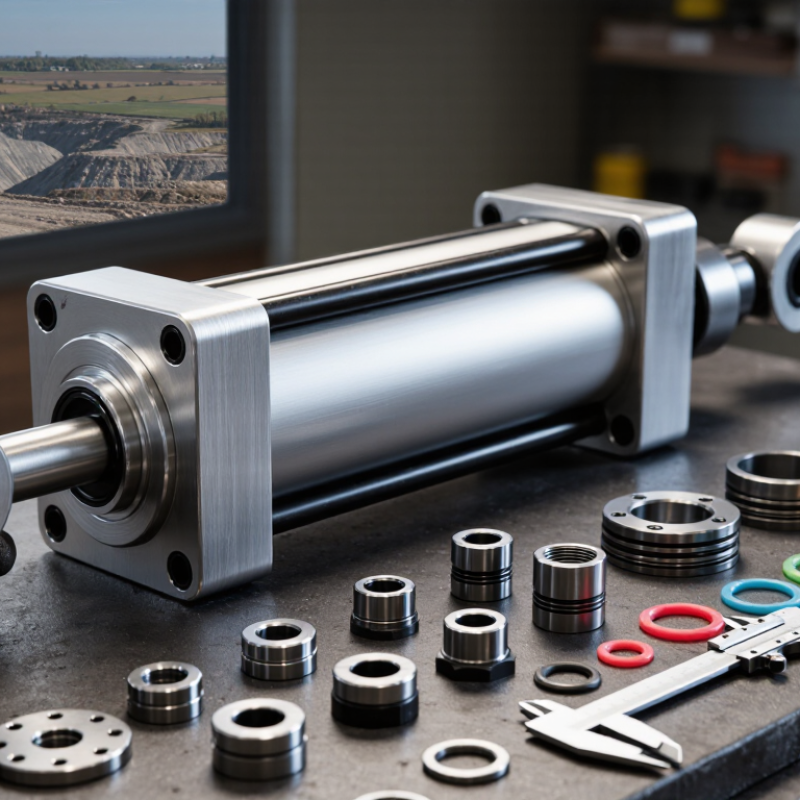
Define Load, Stroke, and Speed with F = P × A and ISO 6020/2 Dimensions
Choosing a special hydraulic cylinder starts with three numbers: load, stroke, and speed. Use F = P × A to estimate bore size, where F is force, P is working pressure, and A is piston area. At 160 bar, a 50 mm bore develops about 31.4 kN theoretically. Real output is lower because of friction, seal drag, and pressure losses. Allow a practical margin of 15–25%. Do not size from peak load alone.
Short strokes need accurate mounting. Long strokes need rod guidance and buckling checks. Calculate speed with v = Q ÷ A, using flow in cubic metres per second. A cylinder requiring 500 mm travel at 100 mm/s needs approximately 19.6 L/min during extension with a 50 mm bore. It sounds simple. It is not. Flow controls, oil temperature, and valve response can change the result.
ISO 6020/2 provides recognized mounting and dimensional guidance for medium-duty cylinders, commonly associated with a 160 bar nominal pressure and 200 bar peak pressure. Confirm the current edition before finalizing dimensions. Industry market reviews continue to forecast steady growth in hydraulic-cylinder demand, while energy-efficiency reports repeatedly identify throttling and leakage as major loss sources. That makes seal condition and circuit design part of cylinder selection. My own weak point is trusting catalogue dimensions too quickly. Check the actual load path, side force, duty cycle, and retraction force. A cylinder may fit the drawing and still fail in service.
| Tip | Selection Dimension | Engineering Check | Illustrative Data | Practical Recommendation |
|---|---|---|---|---|
| 1 | Define the required load | Use F = P × A, where F is force in newtons, P is pressure in N/mm², and A is effective piston area in mm². For a round piston: A = πD²/4. | Bore diameter D = 100 mm Piston area A = 7,854 mm² Working pressure P = 16 MPa Theoretical extension force F = 125,664 N ≈ 125.7 kN | Compare the calculated force with the external load, friction, acceleration, and any tooling resistance. Apply an engineering margin rather than sizing exactly to the nominal load. |
| 2 | Check retraction force | Retraction uses the annular area: Aannular = π(D² − d²)/4, where d is the rod diameter. | Bore D = 100 mm Rod d = 70 mm Annular area = 4,006 mm² At 16 MPa, theoretical retraction force ≈ 64.1 kN | Use the lower rod-side force when the cylinder must pull a load, clamp against resistance, or control a return stroke. |
| 3 | Specify the stroke accurately | Stroke is the linear travel from fully retracted to fully extended. The usable travel should include the machine motion requirement without forcing the cylinder to act as a mechanical stop. | Required machine travel = 500 mm Selected nominal stroke = 500 mm Allowance for external end stops = designed outside the cylinder | Confirm retracted and extended envelope dimensions, mounting-center distance, available space, and whether cushioning is needed near either end of stroke. |
| 4 | Calculate speed and flow | Cylinder speed is approximately v = Q/A, and required flow is Q = v × A. Flow must be calculated separately for the cap end and rod end. | Extension speed = 0.10 m/s Cap-end area = 7,854 mm² Required extension flow ≈ 47.1 L/min Retraction flow at 0.10 m/s ≈ 24.0 L/min | Check pump capacity, valve flow rating, hose size, and pressure loss. Actual speed may be lower because of leakage, compressibility, and circuit restrictions. |
| 5 | Match the mounting and dimensions | ISO 6020/2 provides a standardized dimensional framework for selected metric hydraulic cylinder mounting arrangements. The applicable bore, rod, mounting type, port arrangement, and dimensional series must be verified from the relevant drawing. | Required checks include: • Bore and rod diameter • Retracted length • Mounting-center dimensions • Rod-end thread and attachment • Port size and location | Do not select a replacement by bore and stroke alone. Confirm the complete dimensional drawing and the exact mounting style before fabrication or installation. |
| 6 | Evaluate rod stability and side load | Long strokes, high compressive loads, and poor alignment can increase buckling risk and seal or bearing wear. Hydraulic cylinders should transmit axial force; side loads should be minimized or externally guided. | Risk factors include: • Long unsupported stroke • High compression force • Eccentric load • Misaligned pivots • High impact at end of stroke | Consider a larger rod, intermediate guide support, spherical rod-end alignment, external guides, or a different mounting arrangement when side loading cannot be eliminated. |
| 7 | Specify environment and control features | Temperature, contamination, corrosion, duty cycle, impact, and stopping accuracy affect seals, materials, cushioning, sensors, and surface protection. | Application review: • Ambient temperature: −10 to 50 °C • Frequent cycling: 20 cycles/min • Outdoor moisture exposure • Controlled deceleration required | Specify compatible seals and fluid, corrosion-resistant protection where required, adjustable cushions for high-speed travel, position sensing if feedback is needed, and filtration suitable for the hydraulic circuit. |