For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615
Service & Repairs: 616-698-7500
24/7 Parts: 1-800-727-8780
sale@inlandmachineokc.com
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780

With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.

Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
616-698-7500

Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.

Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.

Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.

Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780Choosing a Pipe Swaging Machine is not simply a matter of finding the highest tonnage or lowest price. The right choice depends on the tube material, outside diameter, wall thickness, required end profile, and daily production volume. Small details matter. A machine that forms thin stainless-steel tubing may not handle thicker carbon-steel pipe reliably, even when its headline capacity looks sufficient.
Industry data shows why careful equipment selection matters. World Steel Association’s World Steel in Figures 2024 reports global crude steel production of 1,892.2 million tonnes in 2023. That figure reflects the scale of metal manufacturing, but it does not tell buyers which machine fits their specific work. The U.S. Census Bureau’s Annual Survey of Manufactures also tracks manufacturing investment, offering useful context for evaluating capital purchases. Neither source replaces testing your own tube samples. That step is easy to overlook.
A practical comparison should examine forming force, stroke length, tooling options, cycle time, changeover effort, and operator controls. Ask suppliers for sample runs using your actual material and dimensions. Inspect the finished ends for cracking, ovality, and consistency—not just appearance. Request written specifications, maintenance requirements, and references from similar production settings. A lower purchase price can look attractive, yet tooling changes or slow setup may raise the real cost per part. There is no perfect machine for every workshop. This guide explains how to compare capacity, accuracy, support, and total ownership cost before choosing a Pipe Swaging Machine.
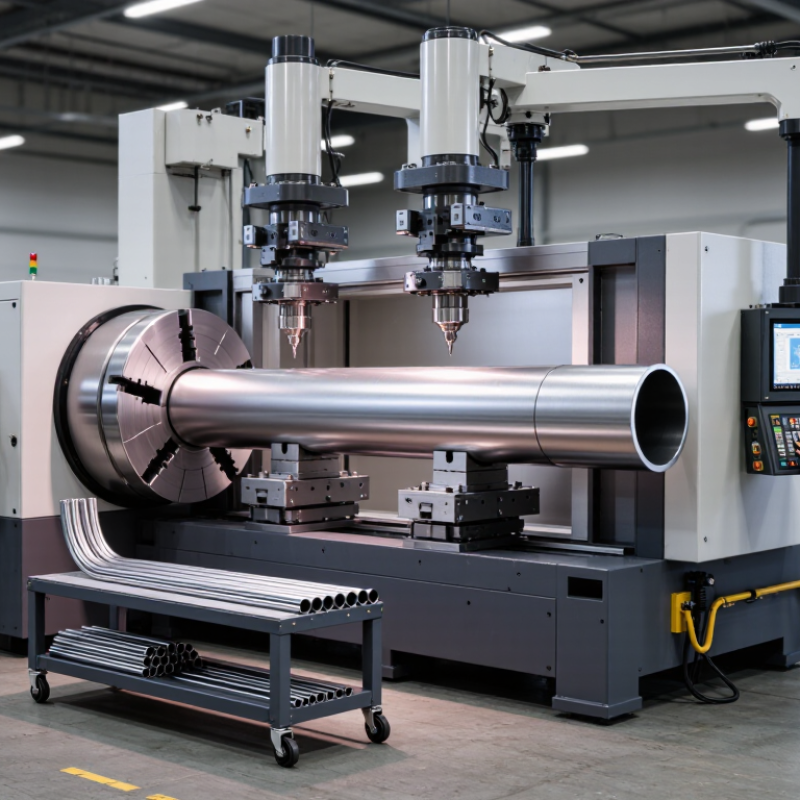
Pipe swaging reduces or reshapes a tube’s end by applying radial pressure through dies. It can form a smaller spigot, a taper, or a smooth transition without adding a separate fitting. In fabrication shops, swaged ends help pipes connect in handrails, heat exchangers, vehicle assemblies, and fluid lines. The result depends on material, wall thickness, and die geometry. Thin-wall tube can wrinkle; harder alloys may spring back. Small changes matter.
Grand View Research valued the global steel pipe market at about US$95.2 billion in 2022. Its report projected a 5.3% compound annual growth rate through 2030.
This describes the wider pipe market, not swaging-machine sales, but it signals the scale of pipe-based manufacturing. When comparing machines, check capacity against the largest diameter and wall thickness you actually process. Also assess repeatability, stroke control, tooling change time, and operator guarding. Request a trial with your own tube, then inspect ovality, surface marks, and finished dimensions. A fast cycle is not enough. I would not choose by tonnage alone; production mix and setup time can quietly outweigh press power. That trade-off is easy to miss.
How to Choose the Best Pipe Swaging Machine? Defining Your Pipe Materials, Sizes, and Production Needs
Start with the actual tube, not just its nominal size. Record material grade, outside diameter, wall thickness, and end-reduction dimensions. Stainless steel may work-harden during forming; softer copper can mark or collapse under excessive pressure. Include seam position and surface finish in your trial. Small details matter.
The World Steel Association’s World Steel in Figures 2023 reports 1,878.5 million tonnes of crude steel production in 2022. That figure describes a vast material supply, not your specific pipe demand. For machine selection, test samples from your own supply lot. Measure springback and inspect for wrinkles, cracks, and ovality. A neat specification sheet can hide a messy tube lot.
Then match capacity to production needs. Compare the machine’s usable diameter range and forming force with your largest, thickest tube—not only your average part. For low-volume work, quick die changes may matter more than peak speed. High-volume lines need repeatable cycles and consistent inspection. Small batches differ. Ask for a run using your material, tooling, and target cycle time. I would not size a machine from nominal diameter alone; that shortcut can fail when wall thickness or alloy changes.
Typical yield strength helps indicate how much forming force a material may require. Compare your material grade and condition before selecting machine capacity.
Illustrative typical values: C12200 annealed copper, 69 MPa; 304 annealed stainless steel, 205 MPa minimum; 6061-T6 aluminum, 276 MPa minimum; and AISI 1018 cold-drawn steel, approximately 370 MPa. Actual properties vary by product form and condition. Required swaging force also depends on tube diameter, wall thickness, reduction, and die design.
Pipe swaging machines differ in motion, force, and control. Rotary swagers use rapidly closing dies to reduce tube diameter in small increments. They suit long, concentric reductions and repeat production. Hydraulic press swagers apply a controlled squeeze, making them useful for localized ends, collars, and larger workpieces. Mechanical machines can cycle quickly, but their tooling and stroke settings need careful setup. The forming method matters too. A mandrel supports the inside diameter; without one, thin-wall tubing may wrinkle or collapse. Small details matter.
Automation is increasingly common across manufacturing. The International Federation of Robotics’ World Robotics 2024 report counted about 4.28 million industrial robots operating in factories worldwide in 2023. That figure does not measure swaging machines, but it highlights why programmable controls and repeatable setups may matter in a production cell. Choose CNC control when parts vary often or dimensions need tight tracking. For steady, high-volume work, a simpler mechanical setup may be more practical. Check sample parts for wall thinning, ovality, and surface marks, then compare cycle time with changeover time. A fast machine can still waste hours if dies are awkward to align. And operators can miss things. Test the actual tube material and wall thickness before committing to tooling.
How to Choose the Best Pipe Swaging Machine?
Rated capacity is only a starting point. Match the machine to the pipe material, outside diameter, and wall thickness you actually process. Check its force and stroke range against your largest and smallest jobs, not just a typical part. A short production trial can reveal ovality, cracking, or inconsistent end dimensions. Fit matters.
Controls affect both repeatability and setup time. A clear display should make pressure, stroke, and cycle settings easy to verify. For recurring jobs, stored settings can reduce setup variation, but operators still need to confirm the correct recipe and tooling. I used to give rated force too much weight; that misses how control and setup shape finished-part quality.
Tooling should cover your required sizes and be practical to change, inspect, and replace. Look for secure die alignment and clear setup instructions. Safety features deserve the same attention: check guarding, interlocks, emergency stops, and safe access during maintenance. Check the guard. Ask to see a full operating cycle, including loading and unloading, before choosing a machine. A feature list is useful, but it cannot show every awkward reach or pinch point on your floor. That detail deserves a second look.
| Assessment Area | What to Measure or Check | Practical Selection Criterion | Why It Matters | How to Verify |
|---|---|---|---|---|
| Workpiece capacity | Tube or pipe outside diameter, wall thickness, length, and material grade. | The rated working range must cover the largest and smallest parts in the production mix—not just the nominal pipe size. | Swaging load depends on material strength, wall thickness, reduction, and tooling; diameter alone does not define capacity. | Submit representative part drawings and material details for a capacity review or sample run. |
| Reduction and finished geometry | Required end diameter, taper, transition length, concentricity, and dimensional tolerance. | Confirm the machine and die design can achieve the specified geometry, including any staged reduction or intermediate annealing requirements. | Excessive reduction in one operation can cause cracking, wrinkles, or out-of-tolerance parts. | Review process limits and inspect trial parts with appropriate gauges or measuring equipment. |
| Production rate | Required parts per hour, operating hours per shift, changeover frequency, and loading method. | Compare demonstrated cycle time, including loading, forming, inspection, and tool changes—not just the machine’s stroke rate. | A high forming speed does not guarantee the required output if handling or setup is the bottleneck. | Request a timed production trial using the intended part and operator workflow. |
| Controls and repeatability | Stroke or position adjustment, speed control, stored recipes, status indicators, and fault diagnostics. | Choose controls that let operators set and repeat validated process parameters with suitable access control and clear fault messages. | Repeatable settings help reduce setup variation, scrap, and dependence on individual operator experience. | Check a demonstration of recipe setup, parameter adjustment, alarm handling, and restart after a fault. |
| Tooling and changeover | Die and guide range, material compatibility, tool availability, changeover time, and setup method. | Confirm tooling is available for every required size and profile, with clear identification and a repeatable alignment procedure. | Correctly matched, maintained tooling supports surface quality, dimensional accuracy, and reliable feeding. | Obtain a tooling list, changeover instructions, maintenance guidance, and replacement lead-time details. |
| Safety features | Point-of-operation guarding, interlocked access, emergency stops, safe setup mode, and lockout provisions. | Verify safeguards suit the actual machine layout and intended tasks, including feeding, tool changes, cleaning, and maintenance. | Swaging equipment has moving and pinch-point hazards; safeguards must be assessed as part of the complete installation. | Review the risk assessment, safety documentation, guarding, and applicable local machinery requirements before operation. |
| Maintenance and support | Routine service intervals, wear parts, lubrication needs, documentation, and technician availability. | Favor a maintainable design with documented service tasks and accessible replacement parts. | Planned maintenance helps preserve accuracy and reduce unplanned downtime. | Review the maintenance schedule, spare-parts list, training options, and service response arrangements. |
| Installation requirements | Floor space, foundation or anchoring, electrical supply, compressed air if required, and noise level. | Match the machine’s documented utility and installation requirements to the available site conditions. | Insufficient utilities or space can delay commissioning and complicate safe operation and maintenance access. | Use the installation drawing and utility schedule to complete a site-readiness check before delivery. |
Choose a pipe swaging machine around the parts your workshop actually makes, not the largest catalog capacity. Record the pipe materials, outside diameters, wall thicknesses, and typical batch sizes. Compare those figures with the machine’s rated range, and confirm which material the rating covers. Steel and softer alloys may need different forming force. Measure twice. Too little capacity can produce uneven ends or require repeated passes. Oversizing is not automatically safer; it can consume floor space and tie up capital.
Match the stroke length and available dies to the end shapes and pipe lengths you handle. Check whether changing dies is straightforward, especially if jobs vary throughout the day. Consider the power supply, machine footprint, operator access, and rated duty cycle. A compact unit may fit a crowded workshop but struggle with frequent heavy work. Ask for clear maintenance intervals and setup guidance, then compare them with your team’s experience. A specification sheet cannot reveal every awkward setup. Leave room for the occasional job that does not fit the usual pattern, but avoid paying for capacity you rarely use.