For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615
Service & Repairs: 616-698-7500
24/7 Parts: 1-800-727-8780
sale@inlandmachineokc.com
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780

With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.

Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
616-698-7500

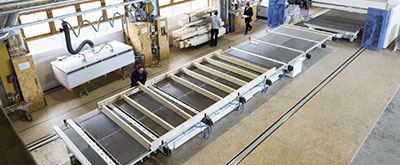
Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.

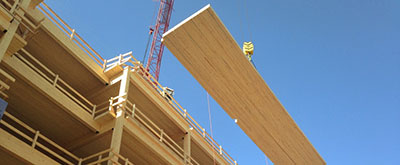
Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.

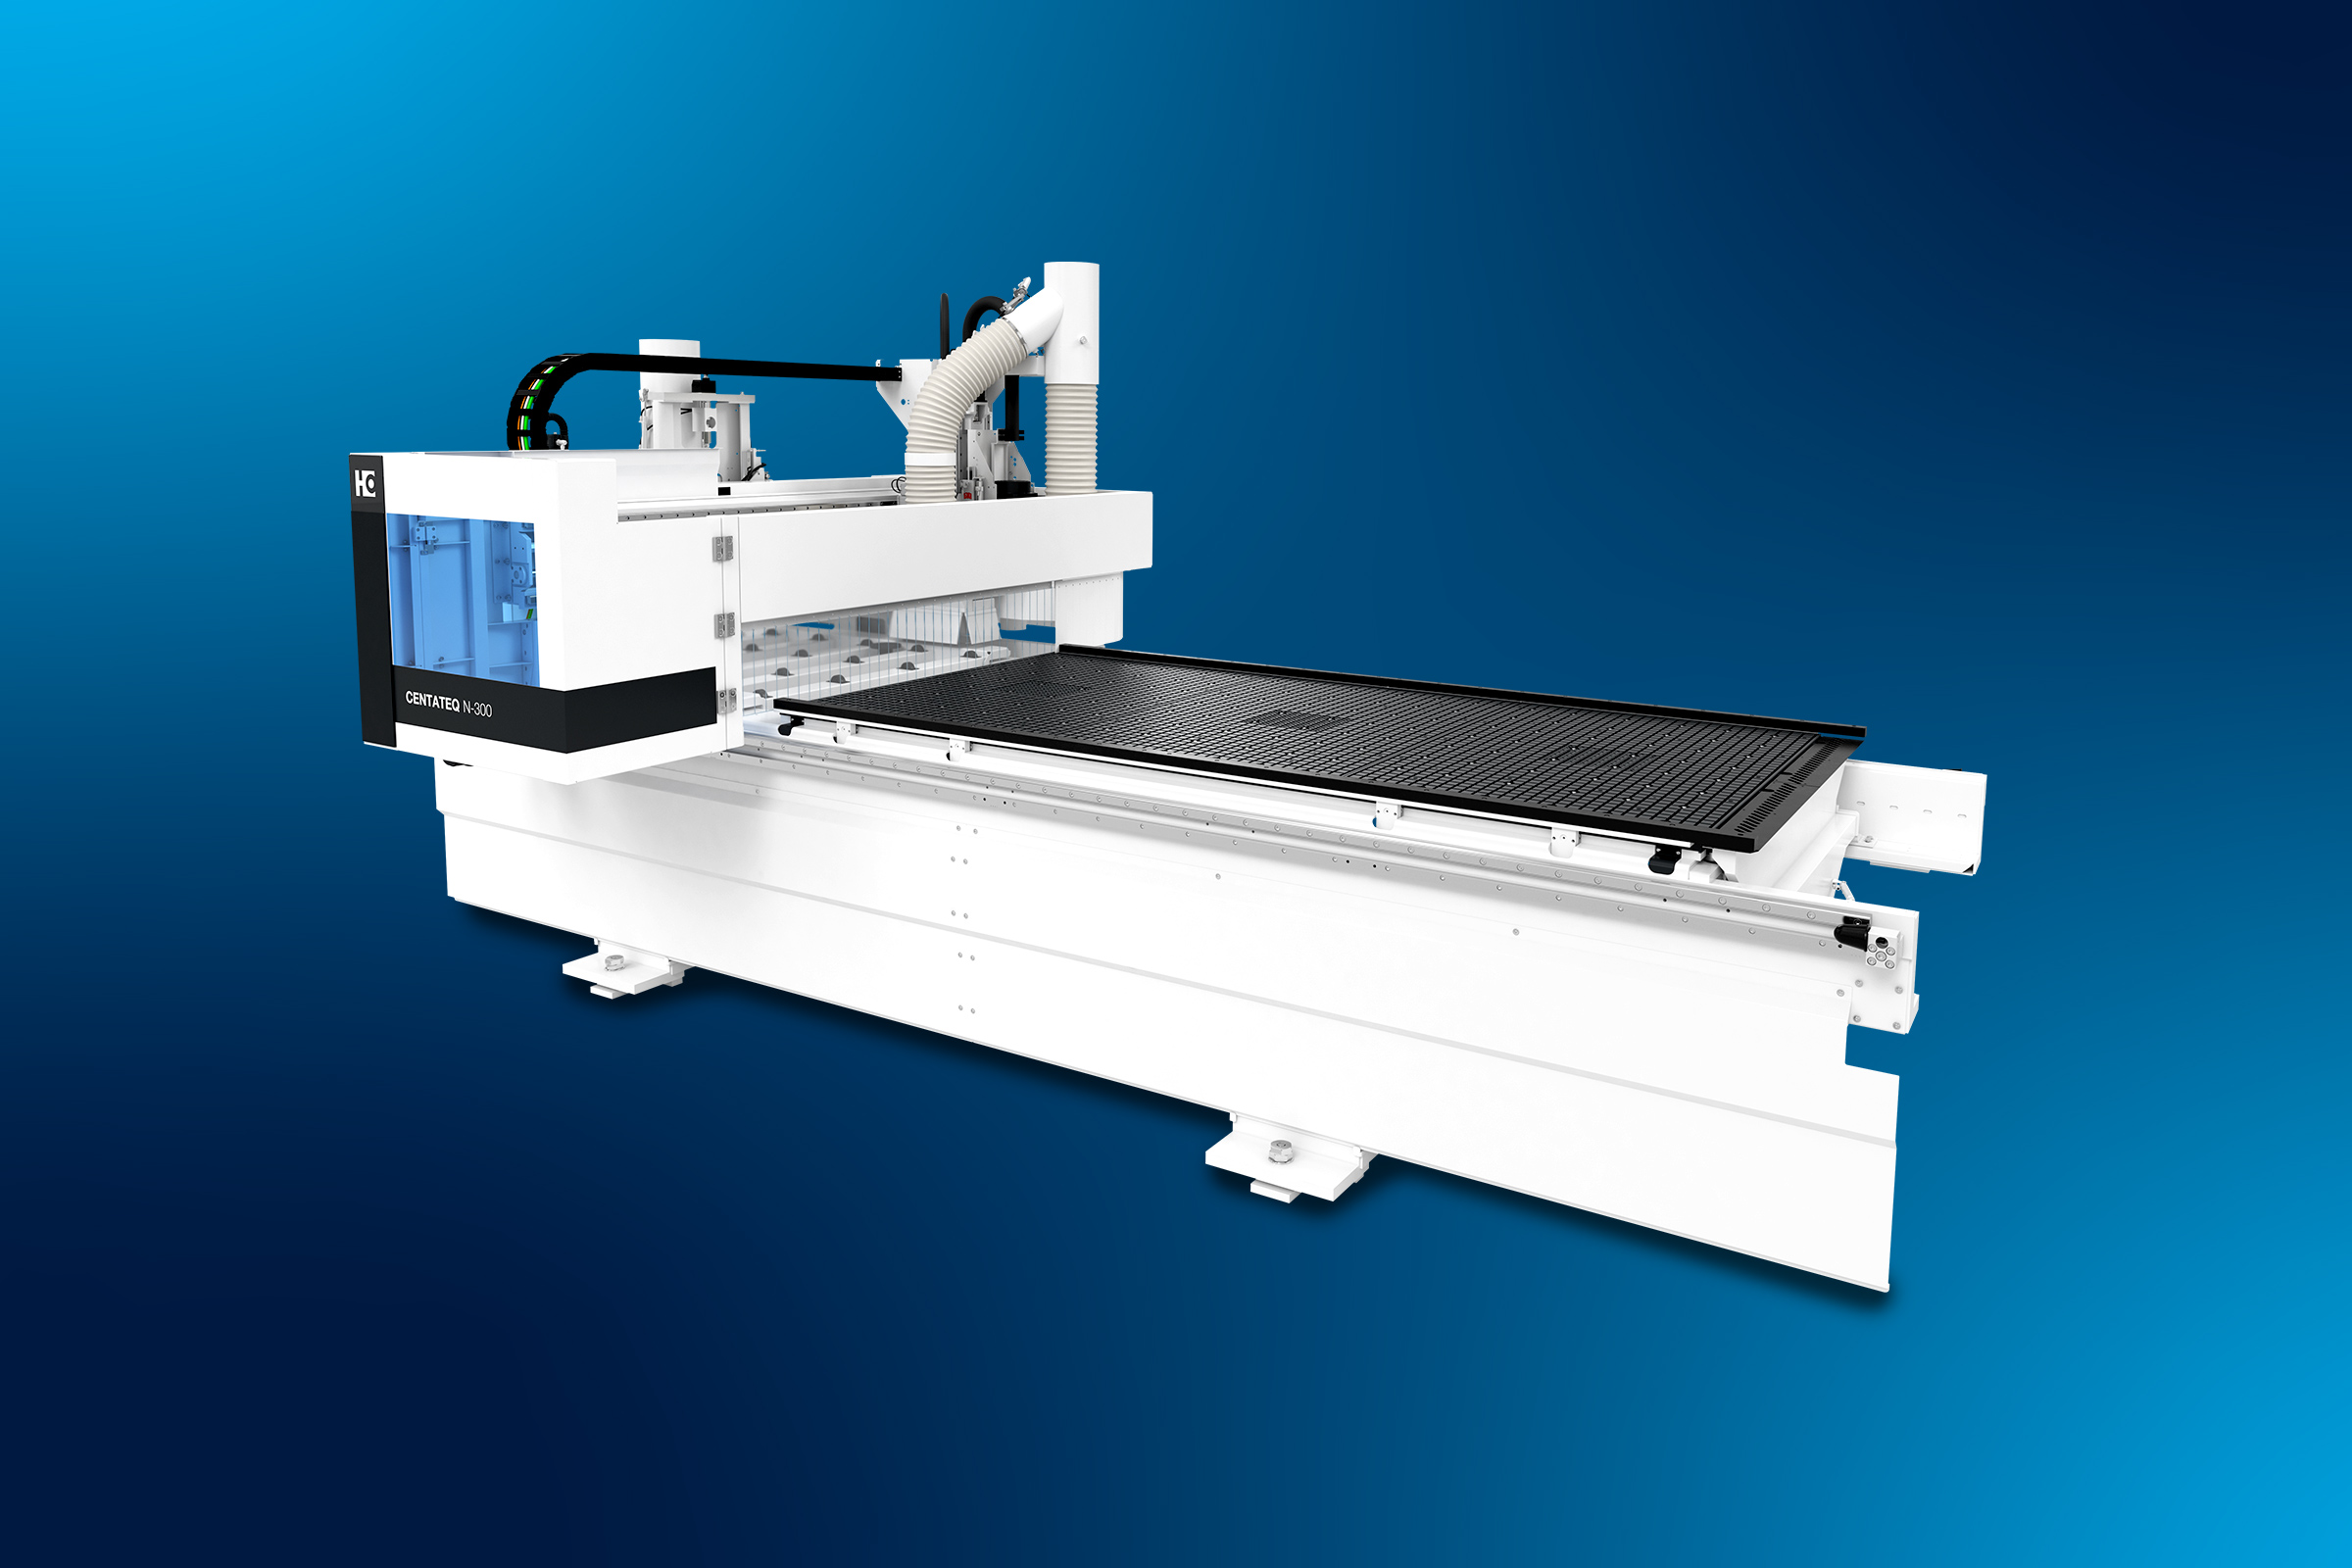
Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.

Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780Choosing the right Laboratory Coating Machine is rarely a simple comparison of speed and price. It is a process decision.
Recent industry reports show strong growth in pharmaceutical manufacturing, battery materials, and advanced functional films. Grand View Research identifies increasing automation and quality control as major equipment-market drivers. MarketsandMarkets also highlights demand for flexible, precise coating systems in research and production environments. These trends matter, but market growth alone cannot select your machine.
Practical evaluation should begin with the coating material and substrate. Check viscosity, solids content, web width, and required wet-film thickness. A 100-millimeter sample may reveal defects that a brochure hides. Edge beading, uneven drying, and trapped bubbles often appear during real trials. They are easy to overlook.
Machine accuracy matters.
Review the coating head, pump stability, drying temperature, line speed, and tension control. For pharmaceutical applications, FDA process-validation guidance supports documented, repeatable manufacturing conditions. For battery and electronic materials, uniform thickness and clean handling can directly affect performance. ASTM test methods may also support thickness, adhesion, and surface evaluation.
Do not judge equipment from one demonstration. Request trial data using your formulation, substrate, and target speed. Compare coating uniformity, cleaning time, energy use, operator workload, and service response. Total cost includes rejected samples and lost development time.
A common mistake is choosing the most advanced configuration. It may be unnecessary. Another is choosing the cheapest machine. That decision can become expensive later. The best Laboratory Coating Machine fits today’s experiments while allowing controlled, measurable upgrades. Reported market figures differ across research firms, so verify assumptions before investing.
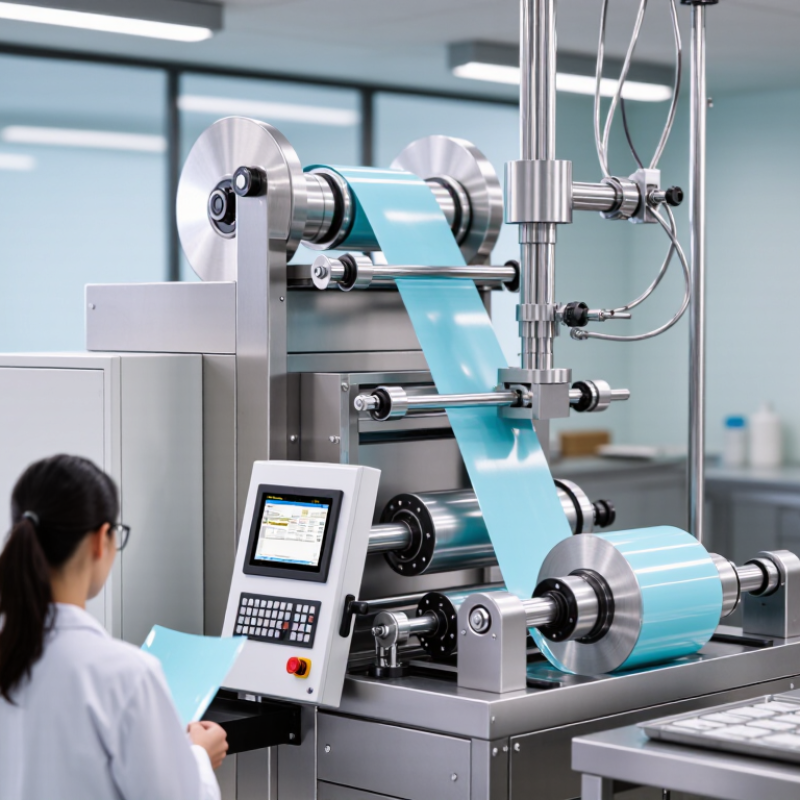
Choosing a laboratory coating machine starts with the substrate, not the machine catalog.
Glass, polymer film, metal foil, and porous paper behave differently under pressure and heat. Flexible films may wrinkle on a rigid vacuum table. Porous paper can absorb liquid before leveling begins. The 2024 Smithers report on flexible packaging identifies thinner films and higher coating consistency as important manufacturing trends. That matters in small trials too.
Measure viscosity at the planned temperature.
Water-like solutions may suit spray or slot-die coating, while 1,000–10,000 mPa·s slurries often need controlled blade pressure. Do not trust one viscosity reading. Shear can change the result. Record spindle, speed, temperature, and waiting time. A practical mistake is selecting a machine from room-temperature data only. Your coating may warm during circulation.
Film thickness and coated area complete the definition.
For a 5–20 μm wet film, use a calibrated gap and stable web speed. ASTM D823 describes controlled drawdown methods for producing uniform films. ISO 4593 provides guidance for measuring plastic-film thickness. For tiny samples, a programmable applicator may provide better repeatability than a pilot coater. For larger panels, examine leveling across the full width. Grand View Research reported continued growth in laboratory automation through 2030, partly driven by repeatable testing and reduced manual variation. Still, automation cannot correct a poorly defined coating task. Measure the wet film, drying shrinkage, edge bead, and final surface. Small details matter.
Choosing a laboratory coating machine starts with the application method, not the purchase price. Drawdown is inexpensive and practical for quick film screening, especially on flat panels. It gives a visible wet-film path, but operator pressure can change thickness. That weakness matters.
Spray application suits textured surfaces and fast coverage. It can reproduce industrial atomization, although overspray may reduce material efficiency. Dip coating offers simple immersion control and useful edge coverage. However, drainage marks and bath contamination require close observation. Spin coating creates very uniform thin films on small, flat substrates. It wastes material at the edge and cannot represent every production geometry. Slot-die coating uses a controlled liquid bead and supports repeatable, continuous films. It demands accurate gap, flow, and substrate alignment.
Data supports investing in repeatability. Grand View Research valued the global paints and coatings market at about USD 206.56 billion in 2023, with projected growth through 2030. MarketsandMarkets projected the laboratory automation market to rise from USD 5.1 billion in 2023 to USD 7.1 billion by 2028. These figures suggest stronger demand for measurable workflows, not merely faster equipment. For comparison, record wet-film thickness, coating speed, viscosity, temperature, and drying conditions. Follow relevant practices such as ASTM D823 for drawdown preparation and ASTM D3359 for adhesion testing. I would not claim one method is universally best. A slot-die system may be excessive for five screening samples, while a drawdown bar may be too limited for scale-up. Test the machine with your actual formulation, substrate, and target thickness. Small surprises reveal more than a polished demonstration.
Laboratory coating machines should be selected around measurable film control, not advertised speed. ASTM D823 provides practices for producing uniform paint, varnish, and lacquer films. It helps technicians compare applicator gaps, drawdown speeds, and substrate preparation. A suitable machine should maintain stable speed, controlled pressure, and repeatable positioning. Small changes matter. A 50-millimeter glass panel can reveal uneven edges, streaks, or pinholes quickly.
ISO 2808 supports film-thickness determination through wet and dry measurement methods. Pair the coating machine with a wet-film comb, precision micrometer, or suitable optical gauge. Record target thickness, actual thickness, temperature, humidity, and drying time. These records create a defensible test trail.
According to Fortune Business Insights’ 2024 market analysis, the global paints and coatings market reached about USD 206.56 billion in 2023. Such scale increases pressure for reliable laboratory screening before production trials.
Choose equipment that allows fine speed adjustment and repeatable gap settings. Automated data capture is useful, but it cannot correct poor specimen preparation. The first setting may fail. That is normal. Review the failed panel instead of hiding it.
Edge buildup may indicate excessive pressure or unsuitable viscosity. Dry-film readings can also mislead when the coating shrinks during curing.
ASTM D823 controls application practice; ISO 2808 verifies the resulting thickness. Used together, they turn machine selection into a controlled measurement decision.
How to Choose the Best Laboratory Coating Machine?
A laboratory coating machine should produce uniform films before adhesion testing begins. Film thickness, coating speed, drying conditions, and substrate preparation can change the result. A reliable machine offers stable speed control, level application, and repeatable pressure. Watch the wet film closely. Uneven edges may reveal poor alignment or excessive applicator pressure.
ASTM D3359 provides a practical 0B–5B adhesion scale. Method A uses an X-cut, while Method B uses a cross-cut pattern for suitable coating thicknesses. After cutting, apply standardized pressure-sensitive tape and remove it consistently. Inspect the grid under good lighting. A 5B rating shows no coating removal. A 4B rating allows less than 5% removal. Lower ratings indicate progressively weaker adhesion, with 0B showing more than 65% removal.
Record the coating machine settings beside every rating. Include substrate type, surface cleaning, film thickness, curing time, blade condition, and test temperature. This evidence makes comparisons more defensible. A machine can repeat motion perfectly, yet the operator may still cut too deeply. That mistake can damage the substrate and distort the rating. We learned this the hard way. One clean-looking panel is not enough. Test multiple panels and investigate unusual results instead of averaging them away. A modest machine with disciplined control often outperforms advanced equipment used carelessly.
| Laboratory Equipment or Configuration | Primary Selection Dimension | Recommended ASTM D3359 Method | Important Control Capability | Validation Record to Capture | ASTM D3359 Adhesion Interpretation | Best Use Case |
|---|---|---|---|---|---|---|
| Machine Selection and Coating-Process Control | ||||||
| Manual film applicator with a rigid drawdown plate | Wet-film uniformity and repeatability | Method B for dry coatings below approximately 125 µm (5 mil). Method A is generally used for thicker coatings. | Controlled application speed, clean substrate, fixed applicator gap, and level coating surface | Applicator gap, application direction, application speed, wet-film thickness, substrate identification, and curing conditions | Use the adhesion result only after the coating has reached the specified cure condition. | Small panels, formulation screening, and comparative laboratory studies |
| Programmable spray-coating system | Spray pressure, atomization, traverse speed, and deposition consistency | Method B for suitable thin-film systems; Method A when the cured coating exceeds the Method B thickness range. | Repeatable spray distance, nozzle movement, material delivery rate, and environmental control | Spray pressure, nozzle type, substrate temperature, coating thickness, number of passes, flash time, and cure schedule | Compare panels produced with the same application and curing parameters before assigning a process preference. | Automotive, protective, and decorative coating development |
| Powder-coating laboratory system with controlled curing oven | Powder deposition and cure-profile repeatability | Method B for cured films below approximately 125 µm (5 mil); use Method A for thicker films where appropriate. | Electrostatic voltage, powder feed rate, film thickness, oven temperature, and time at temperature | Metal substrate preparation, coating thickness, oven set point, actual panel temperature, cure time, and surface defects | Adhesion can be affected by under-cure, over-cure, contamination, or excessive film thickness; record these variables with every result. | Powder formulation comparison and cure-window studies |
| Cross-cut adhesion tester with cutting guide | Cut spacing, blade condition, and consistent cutting pressure | ASTM D3359 Method B, commonly used for coatings below approximately 125 µm (5 mil) | Correct cutter spacing for coating thickness, sharp multi-edge blade, and cuts that penetrate to the substrate | Coating thickness, cutter spacing, substrate, conditioning period, tape identification, and test temperature | Report the percentage of area removed from the cross-cut lattice and assign a 0B–5B classification. | Thin coatings on test panels and routine laboratory quality checks |
| X-cut adhesion tool | Cut depth, cut angle, and tape application consistency | ASTM D3359 Method A, generally used for thicker coatings and field-oriented evaluations | Two intersecting cuts made through the coating to the substrate, followed by standardized tape removal | Coating thickness, cut length and angle, tape dwell time, removal direction, and detached coating area | Report the adhesion classification together with the test method because Method A and Method B are not interchangeable procedures. | Thicker protective coatings and larger coated surfaces |
| Conditioning chamber or controlled laboratory environment | Temperature and relative-humidity stability before testing | Use with either Method A or Method B when a defined conditioning protocol is required by the project specification. | Stable temperature, relative humidity, exposure duration, and specimen placement | Conditioning temperature, relative humidity, duration, panel orientation, and time between removal and testing | Conditioning is not a substitute for the adhesion procedure; it is an additional variable that must be reported. | Moisture-sensitive coatings, durability studies, and process comparisons |
| Digital coating-thickness gauge used with the coating machine | Dry-film thickness verification | Supports ASTM D3359 method selection; it does not determine adhesion by itself. | Gauge calibration, measurement location, substrate compatibility, and repeat measurements | Mean thickness, individual readings, measurement locations, gauge calibration status, and coating uniformity | Thickness must be documented because the applicable D3359 method and cutter spacing depend on the coating system and specimen condition. | Release testing and correlation of thickness with adhesion performance |
| ASTM D3359 Adhesion Classification Reference | ||||||
| 5B | 0% removed | No coating detachment or flaking within the tested area. | Record the test method, specimen condition, coating thickness, and visual result. | Excellent adhesion under the specified ASTM D3359 test conditions. | Suitable reference result for a well-adhered coating system | |
| 4B | Less than 5% removed | Small flakes of coating detached at intersections or along the cuts. | Photograph the tested area when the result is close to an acceptance limit. | Good adhesion with minor detachment. | Often acceptable when the project specification allows limited coating loss | |
| 3B | 5% to 15% removed | Jagged removal along cuts or at intersections, with a noticeable but limited affected area. | Document the affected area and compare with the specified acceptance criterion. | Intermediate adhesion; acceptance depends on the coating specification and application purpose. | Useful warning level for process optimization | |
| 2B | 15% to 35% removed | Coating detachment occurs along cuts and within adjacent areas. | Investigate substrate preparation, cure, contamination, film thickness, and coating compatibility. | Limited adhesion; commonly indicates a need for process investigation. | Failure-troubleshooting and formulation screening | |
| 1B | 35% to 65% removed | Large areas of coating are removed from the tested region. | Repeat only after checking specimen preparation and test execution. | Poor adhesion under the specified test conditions. | Process or coating-system failure investigation | |
| 0B | More than 65% removed | Detachment is greater than 65% of the tested area, including severe flaking or peeling. | Verify that the cuts reached the substrate and that the coating was properly cured before final judgment. | Very poor adhesion under the specified test conditions. | Immediate corrective-action review | |
| Practical Selection Rule | ||||||
| Preferred laboratory setup | Repeatability before automation level | Match Method A or Method B to coating thickness and specimen geometry. | Choose equipment that controls application, curing, thickness, and conditioning—not only coating deposition. | Use a standardized record sheet for every panel and test result. | A robust comparison normally requires the same substrate preparation, coating thickness range, cure schedule, conditioning history, and ASTM D3359 method. | Select the machine that minimizes uncontrolled variables and produces reproducible 0B–5B results. |
How to Choose the Best Laboratory Coating Machine?
A laboratory coating machine should protect people before it protects a process. Check guards, interlocks, emergency stops, and ventilation connections. Ask how operators access the coating chamber during cleaning. Confirm that exposed surfaces tolerate the intended solvents and cleaning agents. Small design details matter. A loose seal can affect safety and coating results.
Calibration deserves equal attention. Verify temperature probes, airflow sensors, spray rate, drum speed, and pressure controls. Request calibration certificates with traceable standards and clear due dates. Test the machine under realistic operating conditions, not only at idle. I once trusted a displayed temperature without checking probe placement. That assumption could have distorted the entire batch record. It remains a useful warning.
Data integrity is central to 21 CFR Part 11 readiness. The control system should use unique accounts, role-based permissions, secure electronic signatures, and automatic audit trails. Records should show who changed a parameter, when, and why. Confirm that timestamps remain consistent and that backups can be restored. Review whether original data stays protected from silent editing. No system is perfect. Operators still need training, documented procedures, and periodic review. A practical evaluation includes challenge tests, such as rejecting an unauthorized setting change or tracing one batch from setup through final report.
Verify safety, calibration, and 21 CFR Part 11 data integrity before equipment qualification and routine use.
This checklist reflects core verification areas: machine safety controls, calibration traceability, electronic-record validation, audit trails, access control, and electronic-signature linkage. Each control should be documented and verified before release.