For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615
Service & Repairs: 616-698-7500
24/7 Parts: 1-800-727-8780
sale@inlandmachineokc.com
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780

With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.

Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
616-698-7500

Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.

Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.

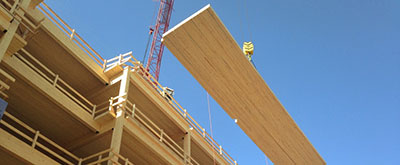
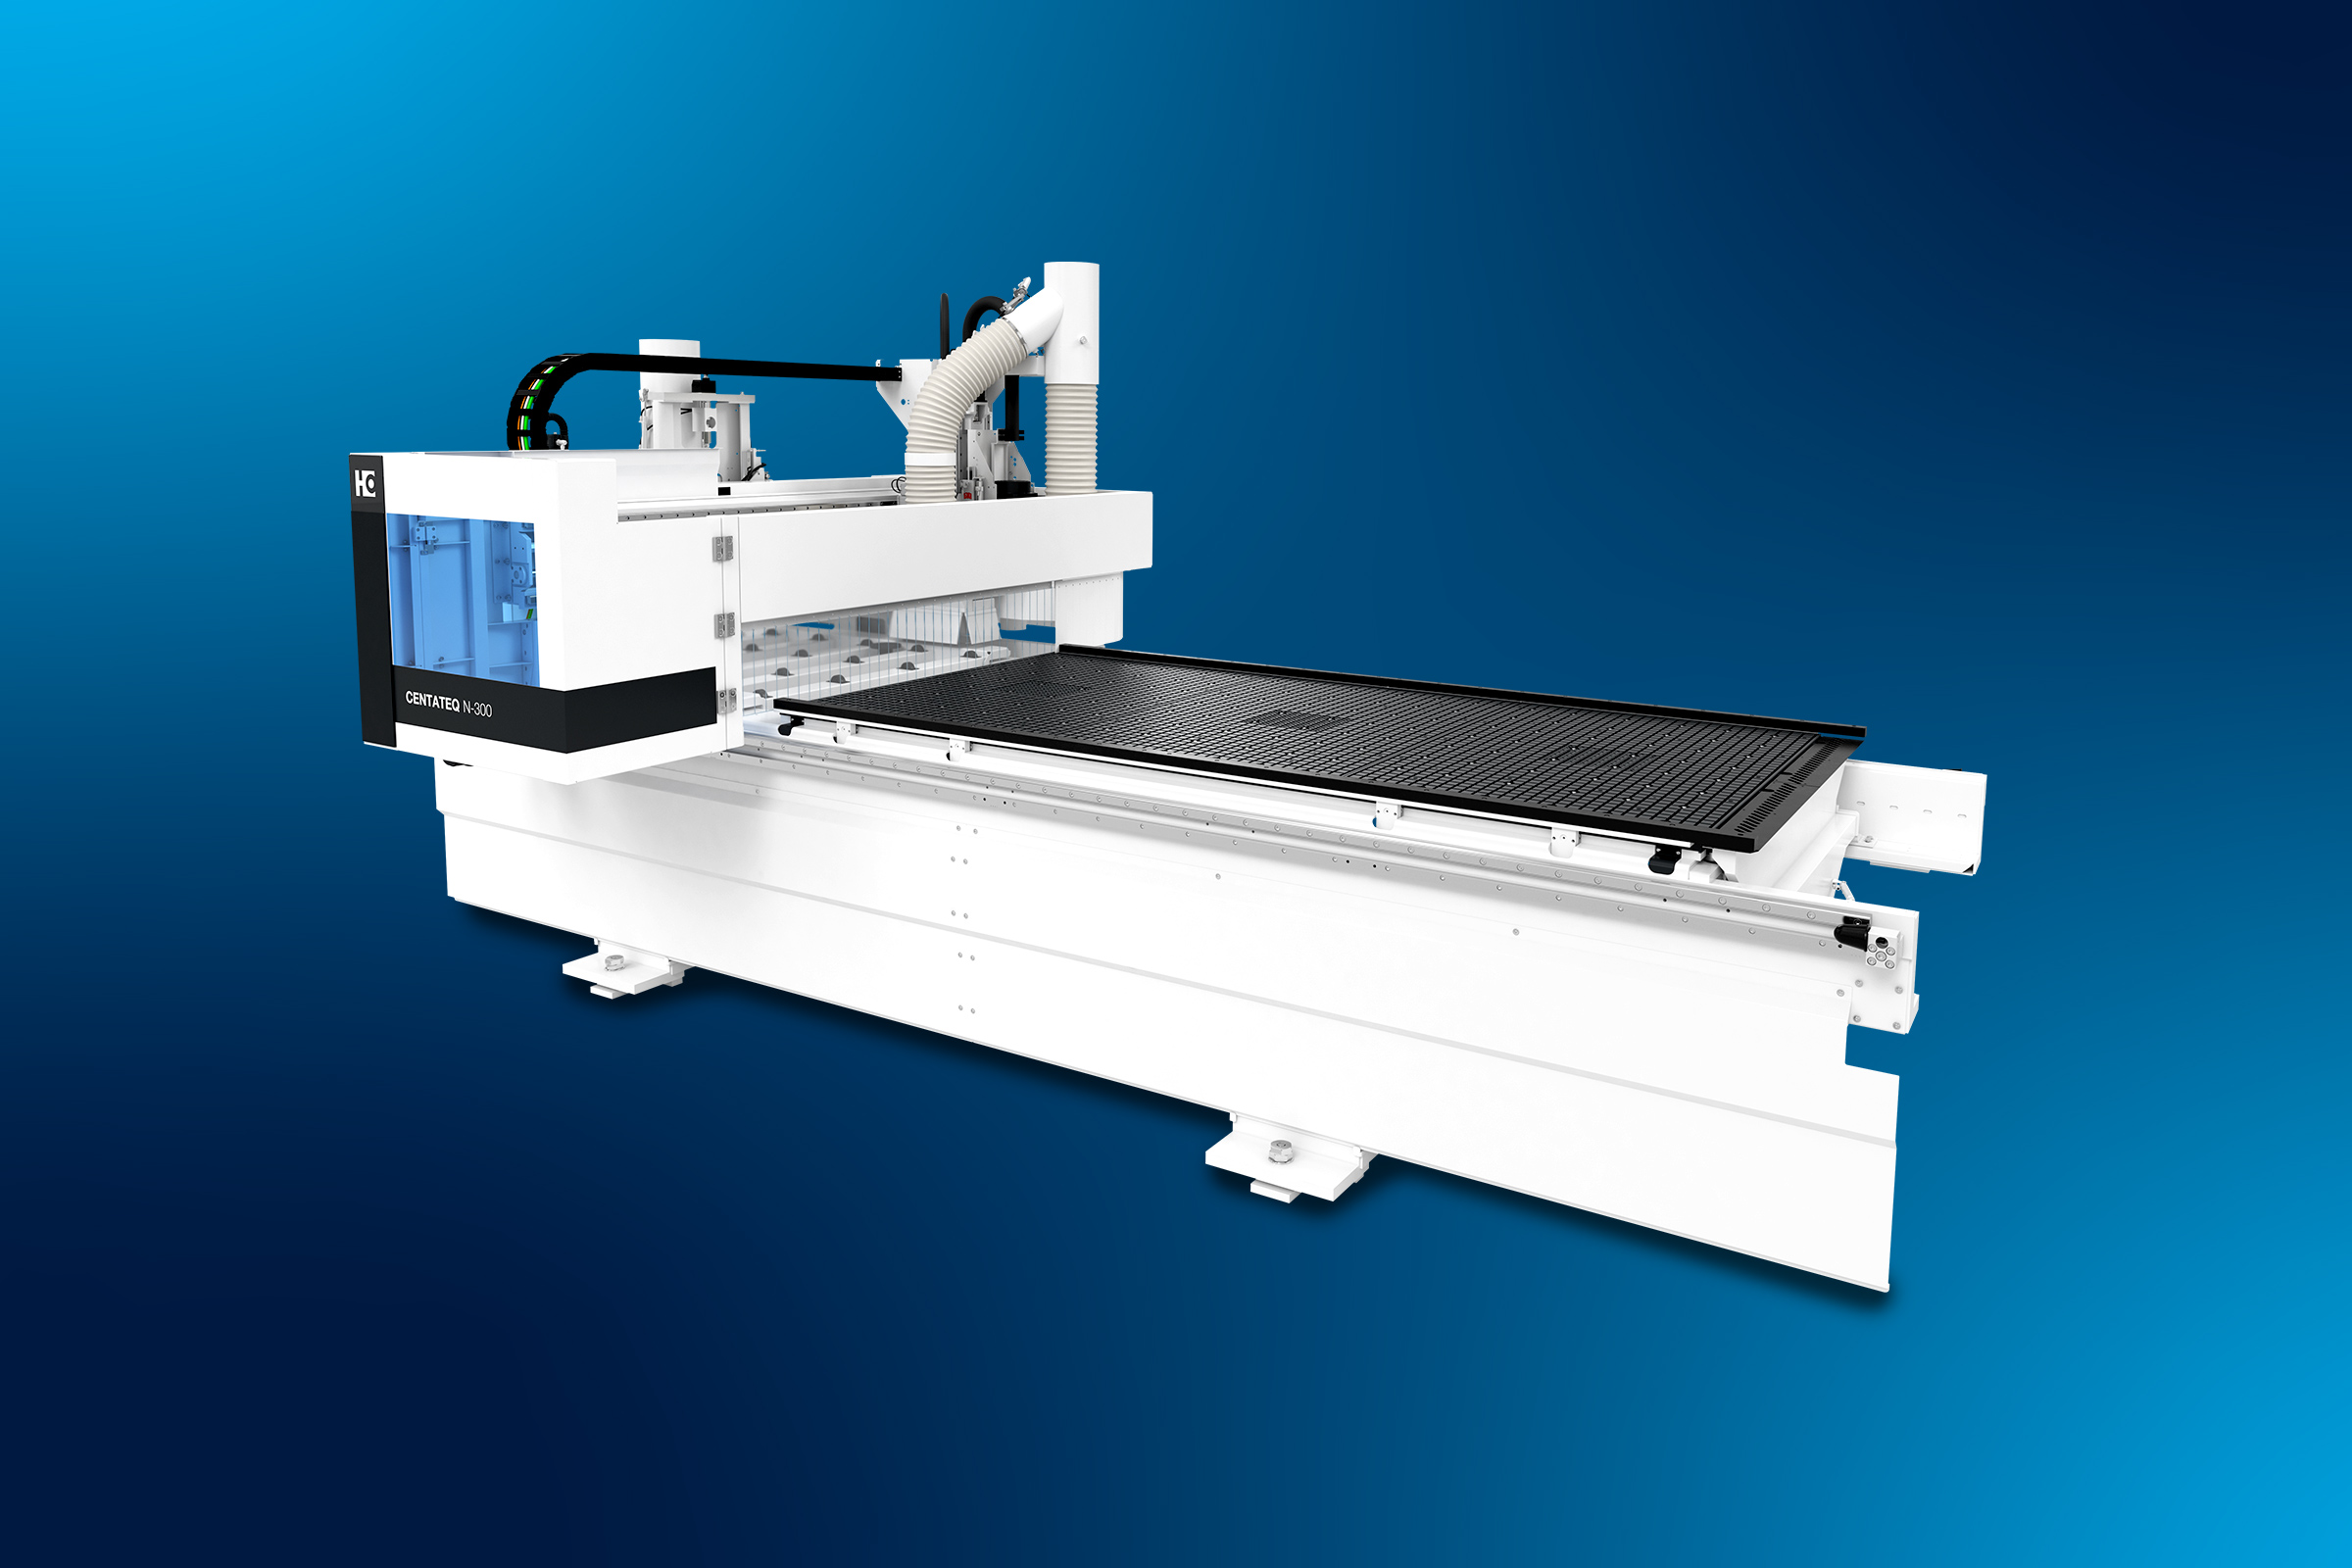
Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.

Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615
Service & Repairs: 616-698-7500
24/7 Parts: 1-800-727-8780
sale@inlandmachineokc.com
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780

With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.

Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
616-698-7500

Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.

Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.

Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.

Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780Choosing a Hole Saw For Metal is not just a matter of matching a diameter to a hole. The metal type, sheet thickness, and expected cut quality all affect the right choice. A thin stainless-steel panel calls for a different approach than a thick mild-steel plate. Small details matter.
Start by checking the hole saw’s construction and tooth design. Bi-metal saws are commonly used for varied workshop tasks, while carbide-tipped models may suit tougher materials or frequent cutting. Check the manufacturer’s specifications before deciding; labels alone do not tell the whole story. Tooth pitch, cutting depth, and arbor compatibility deserve attention too. A saw that fits the drill poorly can wobble, leave a rough edge, or bind. Not ideal.
Speed and heat also shape the result. Metal cutting usually calls for controlled pressure, a suitable drill speed, and cutting lubricant when recommended for the material and tool. Let the teeth do the work. For deeper cuts, clear chips periodically instead of forcing the saw through. Wear eye protection, secure the workpiece, and follow the tool maker’s safety instructions. These steps sound ordinary, but they are easy to skip when a job seems small. This guide explains how to compare hole saw types, sizes, and practical features, so you can choose with fewer surprises. Even careful selection is not perfect; test on scrap when the finish or fit matters.
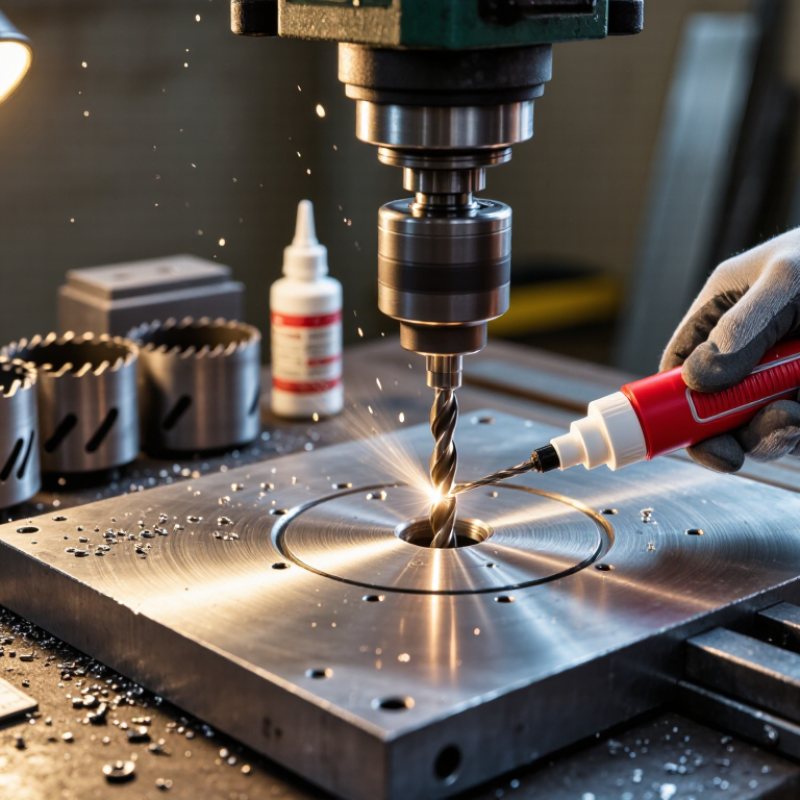
Before choosing a hole saw, identify the metal rather than guessing from its appearance. Mild steel is generally easier to cut than stainless steel, which resists heat and can work-harden. Aluminum cuts readily but may grab the teeth if feed pressure is uneven. Check the workpiece label or ask the supplier when the alloy is unclear. A quick check helps.
Thickness matters just as much. Compare it with the hole saw’s stated cutting depth, and leave room for chips to clear. Thin sheet metal can flex, so clamp it securely against a backing board. For thicker stock, confirm that the saw can cut through in one pass; otherwise, chips may pack into the teeth and heat the tool. Stop and clear them when needed.
Match the saw’s tooth material and cutting speed to the metal. A bi-metal saw is often suitable for mild steel, while harder metals may call for a carbide-tooth model rated for that material. Stainless steel needs steady pressure and cutting fluid to limit heat. Do not force the cut. If the saw squeals, smokes, or stops making progress, pause and reassess the speed, lubrication, and tooth condition. I have found that rushing here usually costs more time later.
For most mild-steel jobs, a bi-metal hole saw offers a practical balance of toughness and cutting life. Its flexible body resists cracking, while hardened teeth handle repeated cuts. For stainless steel or thicker, more demanding work, consider a saw with suitable high-speed steel teeth or carbide tips. Check the tool’s stated material range; not every carbide design suits every metal. Small detail: heat matters. Use a controlled speed and cutting fluid where recommended, and clear chips often so they do not pack into the kerf.
Tooth design affects both cut quality and control. Fine teeth usually suit thin sheet because they engage more points at once and reduce snagging. Coarser teeth can clear chips faster in thicker stock, but may catch if the sheet is poorly supported. Variable-pitch teeth alternate spacing to reduce chatter, which can help when the saw vibrates against a broad metal panel. Keep the workpiece clamped, and let the teeth cut without forcing the drill. I have found that an apparently “faster” tooth pattern can leave a rougher edge when the setup is loose. Match tooth pitch to material thickness, then make a test cut on scrap when the finish matters.
Measure the finished opening, not just the fastener or pipe that will pass through it. A hole saw’s stated diameter is usually close to the cut size, but runout and tooth wear can affect the result. For a close-fitting part, check the required clearance and test on scrap of similar metal. A few millimeters matter.
Check the saw’s usable cutting depth against the thickest material you need to cut. Do not confuse the cup’s overall height with its cutting depth; the pilot bit and arbor may also limit access. For a thick plate, confirm the teeth can pass through before the saw body bottoms out.
If the workpiece is layered, include every layer and any gap between them. This is easy to misjudge, so measure twice. For a blind opening, allow room for the pilot bit without drilling deeper than needed.
Clamp the metal firmly, use suitable cutting fluid, and clear the metal slug only after the tool stops. A smaller saw is not always safer; choosing the correct diameter and depth makes the cut more controlled.
Check that the drill can handle the hole saw’s diameter and cutting load. The arbor shank must fit the chuck securely, with no wobble when tightened. Large hole saws need substantial torque, so a compact drill may stall or twist in your hands. A side handle helps control it. Check the drill manual and hole saw instructions for suitable speed ranges and operating limits.
Metal thickness and type affect how the cut behaves. Clamp the workpiece firmly; even a small sheet can catch and spin. Use the recommended pilot bit and cutting fluid, and keep the saw aligned as the teeth engage. Let the teeth do the work instead of forcing the drill. Stop if the saw chatters, binds, or becomes unusually hot. I’ve noticed it is easy to focus on diameter and overlook the arbor fit; that small check can save a frustrating setup.
Tips: Confirm chuck capacity, arbor fit, drill torque, and the specified speed before cutting. Wear eye protection, and clear sharp metal chips with a brush—not your bare hand.
When choosing a hole saw for metal, compare durability by matching the tooth material to the job. Bi-metal saws suit occasional holes in sheet steel and thinner tubing. Carbide-tipped models often last longer in abrasive or thicker material, but they cost more and can chip if pushed sideways. Check the stated cutting depth and replacement-pilot-bit availability, too. A low purchase price is not good value if the teeth dull after a few holes. Count usable cuts, not just the shelf price.
Safety features matter just as much. A secure arbor, a sharp pilot bit, and a design that releases the cut slug can make work steadier. Clamp the workpiece, wear eye protection, and follow the tool maker’s speed guidance. The U.S. Bureau of Labor Statistics recorded 2.8 million nonfatal workplace injuries and illnesses in private industry in 2022. That figure is not specific to hole saws, but it is a useful reminder: metal chips and a snagging cutter deserve respect. Even experienced operators can rush.
Tips: Use cutting fluid when the saw and work material call for it. Start slowly, keep the saw square, and clear chips before they pack around the teeth. If cutting feels rough, stop and inspect the teeth, arbor, and workpiece instead of leaning harder. A cheaper saw may be enough for one clean hole; repeated production usually rewards durability. The trade-off is not always obvious.