-
-
-
-
-
-
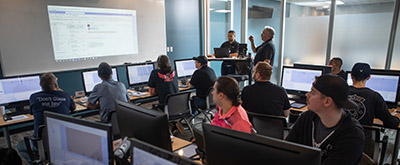
With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.
-
Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
-
-
-
Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.
-
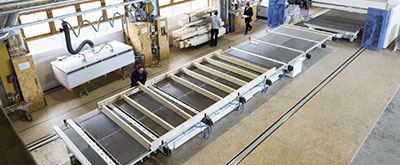
Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.
-
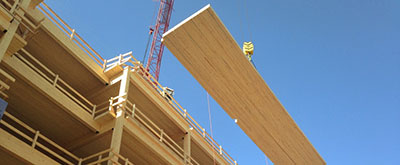
Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.
-
Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
-
-
-
-
-
-
-
With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.
-
Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
-
-
-
Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.
-
Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.
-
Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.
-
Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
-
China Best MCB Inspection Conveyor Manufacturer?
Choosing the China Best Mcb Inspection Conveyor Manufacturer requires more than comparing prices and catalog photos. A reliable supplier should understand miniature circuit breaker production, inspection accuracy, and continuous factory operation. The right Mcb Inspection Conveyor can check appearance, terminal position, label quality, assembly completeness, and mechanical dimensions. It should also connect smoothly with testing stations and packaging equipment. Small details matter. Guide rails must hold each MCB firmly without scratching its housing. Sensors should detect missing products before they enter the next process.
Experienced manufacturers usually provide layout drawings, sample trials, and documented inspection procedures. Their engineers should explain camera resolution, conveyor speed, reject methods, and data traceability in practical terms. A factory visit or live video audit can reveal important details, including cable routing, spare parts storage, and operator access. Factory acceptance testing is useful, while site acceptance testing confirms real production performance. Ask for measurable results, not only polished promises. No conveyor is perfect. Even a well-designed system may need adjustment when product tolerances change or dust enters the inspection area.
This article outline will examine how to evaluate Chinese suppliers through engineering capability, customization experience, quality control, and after-sales support. It will also discuss lead time, maintenance access, software usability, and integration risks. A dependable manufacturer should welcome technical questions and admit reasonable limitations. That honesty often matters more than impressive marketing language. The best choice is not simply the cheapest machine, but a stable inspection solution that protects product consistency and supports long-term production efficiency.
What Is an MCB Inspection Conveyor?
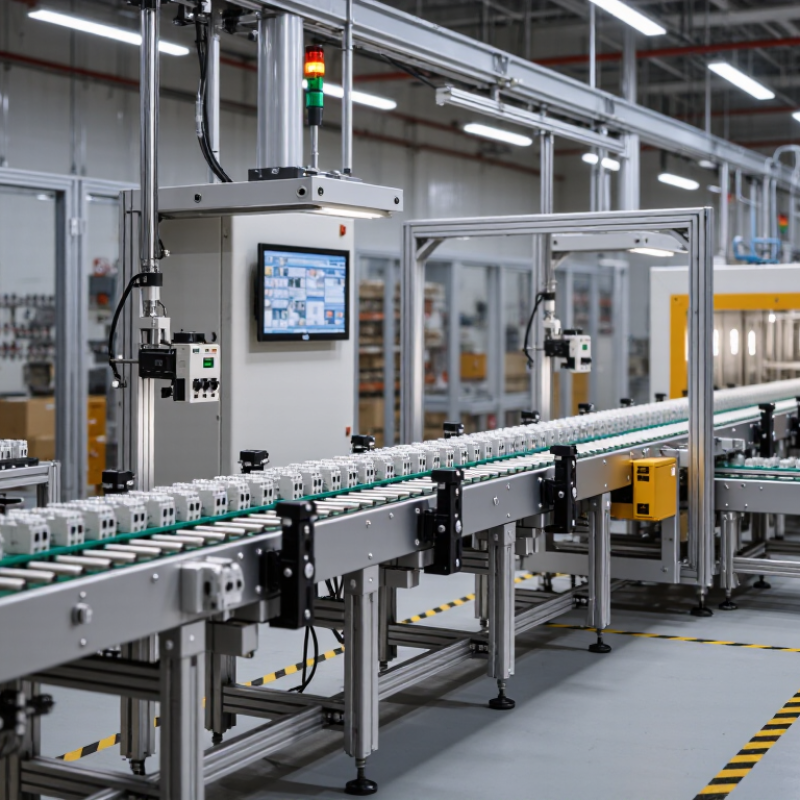
An MCB inspection conveyor is an automated system that moves miniature circuit breakers through controlled inspection stations. It keeps each unit aligned, spaced, and visible for testing. Unlike a simple transport belt, it may combine indexing mechanisms, cameras, sensors, and electrical test modules. The conveyor records inspection results against production data, helping operators locate defects quickly. Typical checks include housing damage, missing components, terminal position, label quality, and switching movement.
In practical use, stable positioning matters greatly. A loose product can shift under a camera and create a false result. Guide rails, adjustable fixtures, and gentle stopping cylinders reduce this risk. Vision sensors examine small details, while presence sensors confirm that every cavity contains an MCB. Some systems also perform continuity, insulation, or mechanical operation tests through controlled contacts. Test limits should follow approved technical requirements and documented quality procedures.
Yet inspection is never flawless. Dust may confuse a camera. Vibration can affect contact testing. An experienced technician should review rejected samples instead of trusting every automatic decision. I would also check lighting, belt tension, sensor alignment, and stored data during routine maintenance. These details seem minor. They are not. A reliable conveyor needs clear rejection logic, guarded moving parts, emergency controls, and repeatable results across different shifts. Its design should match the MCB size, production speed, inspection depth, and available operator skills.
China Best MCB Inspection Conveyor Manufacturer? - What Is an MCB Inspection Conveyor?
| Data Dimension | Typical Data or Range | Inspection or Conveyor Relevance |
|---|---|---|
| Equipment Definition | Automated conveying and inspection system for miniature circuit breakers (MCBs) | Moves MCBs between assembly, testing, visual inspection, rejection, and packing stations. |
| Typical Product Type | Single-pole, two-pole, three-pole, or four-pole MCB assemblies | The conveyor fixture should match the product width, pole configuration, and housing geometry. |
| Common Product Width | Approximately 17.5 mm per pole for many modular DIN-rail devices | Useful for determining fixture pitch, guide-rail spacing, and multi-pole product handling. |
| Conveyor Structure | Belt conveyor, chain conveyor, indexing conveyor, or custom fixture conveyor | Indexing and fixture conveyors generally provide better positioning accuracy for camera and electrical tests. |
| Usable Conveyor Width | Commonly 80–300 mm, depending on product layout and lane quantity | Wider conveyors can support multiple lanes, while narrow conveyors reduce footprint and handling distance. |
| Typical Line Speed | Approximately 5–30 m/min for inspection applications | Actual speed depends on inspection cycle time, product spacing, indexing distance, and required accuracy. |
| Indexing Accuracy | Typically within approximately ±0.2–0.5 mm when using a dedicated indexing mechanism | Stable positioning helps cameras and probes inspect the same product area consistently. |
| Visual Inspection Items | Housing damage, missing components, incorrect assembly, label presence, terminal condition, and lever position | Machine vision can identify visible defects and verify product presence or orientation without manual handling. |
| Dimensional Inspection | Overall length, width, height, terminal position, and component alignment | Laser sensors, displacement sensors, or cameras can be integrated for non-contact dimensional checks. |
| Electrical Inspection | Continuity, insulation resistance, dielectric withstand, contact resistance, or functional tests | The conveyor positions the MCB and transfers it to test probes or dedicated electrical test fixtures. |
| Barcode or QR-Code Reading | Optional fixed-mount or smart-camera code reader | Supports product traceability, model verification, production recording, and test-result association. |
| Product Spacing | Commonly 20–100 mm between inspection positions | Spacing must prevent product collision and provide sufficient time for image capture and testing. |
| Reject Handling | Pneumatic pusher, servo-driven actuator, diverter, or stop-and-remove mechanism | Automatically separates failed MCBs from approved products and can record the rejection reason. |
| Control System | PLC with touchscreen HMI, sensors, motor controller, and safety circuit | Provides sequence control, alarm management, recipe selection, speed adjustment, and production statistics. |
| Detection Sensors | Photoelectric sensors, proximity sensors, vision cameras, and encoder feedback | Detects product arrival, position, orientation, blockage, and conveyor movement. |
| Frame Material | Powder-coated carbon steel or stainless steel; aluminum profiles may be used for lighter structures | Material selection depends on cleanability, corrosion resistance, load requirements, and factory conditions. |
| Typical Working Height | Approximately 750–1,100 mm, adjustable according to the production line | The height should align with upstream and downstream equipment and support safe operator access. |
| Power Supply | Common industrial supplies include 220–240 V AC or 380–415 V AC; control circuits often use 24 V DC | The final electrical design must match the installation site and comply with applicable local requirements. |
| Safety Features | Emergency-stop buttons, protective covers, interlocked doors, overload protection, and safety sensors | Safety functions reduce risks from moving parts, electrical testing, unexpected starts, and product jams. |
| Data Output | Pass/fail results, production count, rejection count, alarm history, and traceability records | Data can support quality analysis, process improvement, maintenance planning, and production reporting. |
| Selection Criteria | Product dimensions, required throughput, inspection items, accuracy, layout, integration, and safety requirements | A suitable conveyor is normally designed around the MCB model range and the complete production process. |