For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615
Service & Repairs: 616-698-7500
24/7 Parts: 1-800-727-8780
sale@inlandmachineokc.com
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780

With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.

Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
616-698-7500

Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.

Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.

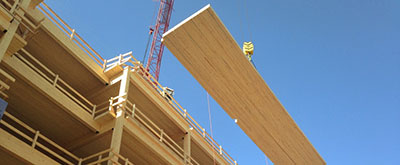
Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.

Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615
Service & Repairs: 616-698-7500
24/7 Parts: 1-800-727-8780
sale@inlandmachineokc.com
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780

With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.

Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
616-698-7500

Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.

Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.

Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.

Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780Compressed air is easy to overlook until a production line slows, a pressure drop triggers alarms, or a compressor runs hot beside a dusty workshop floor. The U.S. Department of Energy’s Improving Compressed Air System Performance: A Sourcebook for Industry identifies compressed air as a significant industrial energy user, accounting for about 10% of electricity used in manufacturing. That makes compressor choice an operating decision, not just a purchase.
A Fixed Speed Screw Compressor can suit facilities with steady air demand, predictable shifts, and limited load variation. Its appeal is straightforward: reliable output and a familiar operating pattern. But constant-speed machines may use more energy when demand falls, so the right choice depends on actual air consumption, not a brochure’s headline capacity. The DOE sourcebook recommends examining the whole compressed-air system, including controls, leaks, pressure requirements, and maintenance. Small details matter. A poorly sized receiver or a neglected filter can undermine an otherwise capable unit.
This guide compares seven fixed-speed screw compressors for industrial use, focusing on practical factors such as airflow, working pressure, motor power, service access, noise, and lifecycle costs. Manufacturer specifications are useful, but they do not replace a site assessment or verified performance data. No shortlist fits every plant. That is worth admitting. Before choosing, operators should match compressor output to measured demand and confirm local service support. The best model is the one that performs consistently under real working conditions—not merely on paper.
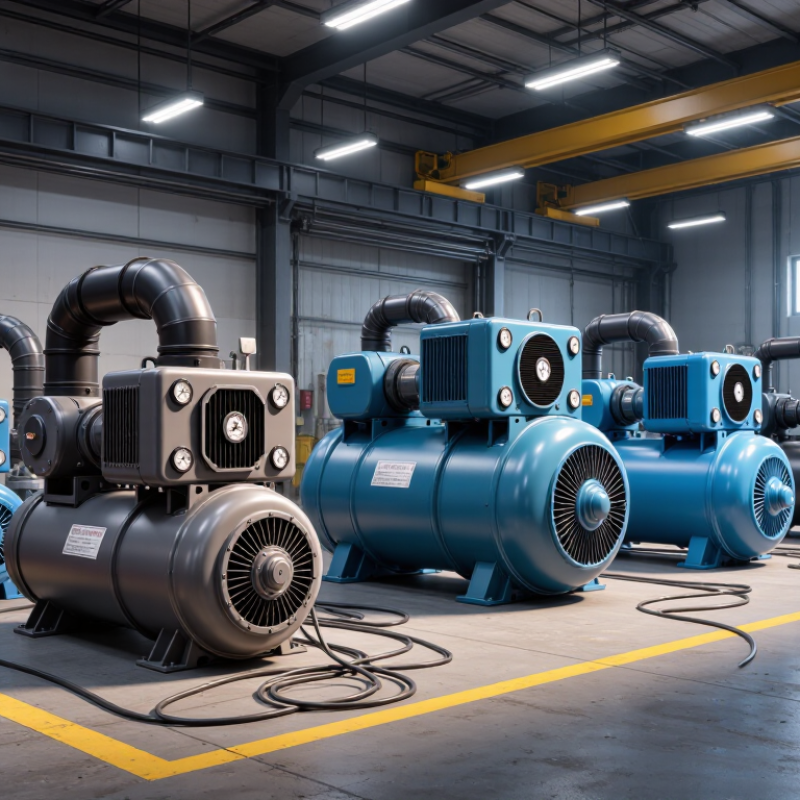
Fixed-speed screw compressors maintain steady motor rotation, giving production lines a predictable air supply. Their rotors compress air continuously while an inlet valve adjusts intake during changing demand. This design suits plants with stable loads, such as packaging, machining, and assembly areas. The U.S. Department of Energy reports that compressed-air systems may consume about 10% of industrial electricity. Small control losses can therefore become expensive.
Constant speed does not mean constant useful airflow. When demand falls, the compressor may unload, vent, or cycle. That transition can waste power and create pressure swings. DOE guidance also indicates that leaks can waste 20–30% of compressor output. A quiet hiss near a coupling may represent a serious annual cost. ISO 11011 recommends measuring pressure, flow, temperature, and energy before system improvements. Real field checks matter more than catalog figures.
A practical selection starts with the plant’s measured average and peak demand. Oversizing often increases unloaded running time. Undersizing causes pressure drops during tool startup. Compressed Air Challenge training materials commonly emphasize leak control, storage, and pressure management together. They are not optional extras. I have seen operators raise system pressure to solve a distant pressure problem, then pay for the mistake through higher energy use. That approach feels convenient, but it deserves reconsideration. A fixed-speed unit performs best when demand remains reasonably steady, receiver capacity is adequate, and maintenance keeps filters, separators, and valves clean.
Selecting the seven best fixed-speed screw compressors starts with verified industrial ratings, not brochure horsepower. ISO 1217 defines how Free Air Delivery (FAD) is measured under stated inlet, discharge, and temperature conditions. That detail matters. A unit rated at 10 bar may deliver less air at 13 bar, while its electrical demand still rises. Compare FAD in m³/min or cfm at the same pressure.
For plants operating between 7 and 13 bar, prioritize stable output, service access, and motor efficiency. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that compressed air can consume about 10% of industrial electricity. It also identifies leakage as a major waste source, commonly reaching 20–30% of compressor output in poorly maintained systems. A 7-bar workshop system therefore needs disciplined leak surveys, correct pipe sizing, and realistic peak-demand calculations. Oversizing is common. It can create inefficient unloaded running.
The strongest candidates usually combine a documented ISO 1217 FAD test, a reliable separator, and controls suited to continuous duty. Check performance at both 7 and 13 bar, not only the best-case point. Record inlet temperature and altitude during acceptance testing. Real factories are rarely laboratory-clean. Dust, heat, and neglected filters can reduce capacity. I would also question unusually high efficiency claims without test conditions, because one missing detail can change the buying decision.
| Rank | Reference Configuration | Motor Rating | ISO 1217 FAD | Rated Pressure | Specific Power | Noise Level | Approx. Package Size (L × W × H) | Best Industrial Application |
|---|---|---|---|---|---|---|---|---|
| 1 | Compact fixed-speed screw package | 7.5 kW | 1.10 m³/min | 7.5 bar(g) | 6.82 kW/(m³/min) | 64 dB(A) | 1,000 × 650 × 1,050 mm | Small workshops, light assembly and intermittent pneumatic tools |
| 2 | Standard-duty fixed-speed screw package | 11 kW | 1.60 m³/min | 8 bar(g) | 6.88 kW/(m³/min) | 65 dB(A) | 1,150 × 700 × 1,180 mm | General manufacturing, maintenance plants and machine shops |
| 3 | Medium-capacity production compressor | 15 kW | 2.35 m³/min | 8 bar(g) | 6.38 kW/(m³/min) | 67 dB(A) | 1,350 × 800 × 1,300 mm | Packaging lines, textile equipment and continuous workshop demand |
| 4 | Heavy-duty factory air compressor | 22 kW | 3.50 m³/min | 8 bar(g) | 6.29 kW/(m³/min) | 69 dB(A) | 1,600 × 900 × 1,500 mm | Automotive components, fabrication and multi-machine production |
| 5 | High-output fixed-speed screw package | 30 kW | 5.00 m³/min | 10 bar(g) | 6.00 kW/(m³/min) | 70 dB(A) | 1,850 × 1,050 × 1,700 mm | Large air networks, CNC production and high-duty pneumatic systems |
| 6 | Central-plant industrial compressor | 45 kW | 7.20 m³/min | 10 bar(g) | 6.25 kW/(m³/min) | 72 dB(A) | 2,200 × 1,200 × 1,900 mm | Foundries, metalworking plants and centralized compressed-air rooms |
| 7 | High-pressure industrial screw package | 75 kW | 11.80 m³/min | 13 bar(g) | 6.36 kW/(m³/min) | 75 dB(A) | 2,800 × 1,450 × 2,150 mm | Heavy manufacturing, process-air systems and long-distance air distribution |
A useful comparison of seven fixed-speed screw compressor choices starts with motor power, but kilowatts alone do not show how much air reaches the tools. As a rough screening guide, a 7.5 kW unit may deliver about 0.8–1.1 m³/min, while an 11 kW model may provide 1.2–1.6 m³/min. A 15 kW option often falls near 1.6–2.2 m³/min. These ranges shift with operating pressure and compressor design, so verify FAD at the required pressure.
For larger demand, typical reference points are 22 kW at roughly 2.4–3.3 m³/min, 30 kW at 3.4–4.5 m³/min, and 37 kW at 4.2–5.6 m³/min. A 55 kW choice may reach around 6.0–8.0 m³/min. Check the test conditions behind every figure. A higher quoted flow is not automatically better if the plant rarely uses it.
Duty matters just as much. Fixed-speed machines suit steady production lines, such as a packaging area running through a long shift. They can cycle inefficiently when demand swings sharply. Watch the load and unload pattern, and compare measured air use with the compressor’s FAD. Small leaks can distort that picture. I would leave some capacity margin, but not choose a much larger motor by habit. That judgment can be wrong without real demand data.
Seven reference configurations compared by motor power, free air delivery, and continuous-duty capability.
Free air delivery (FAD) values are representative industrial ranges measured at approximately 7.5 bar(g). Fixed-speed rotary screw compressors are commonly designed for continuous operation, although actual energy efficiency depends on load profile, unloading time, pressure settings, and system demand.
For fixed-speed screw compressors, specific power is a practical comparison: package input power in kW divided by delivered flow in m³/min. Lower values generally mean less electricity for the same output. Compare units at the same discharge pressure, inlet conditions, and measurement boundary. A machine rated at 7 bar cannot be fairly compared with one tested at a different pressure.
The Compressed Air and Gas Institute’s performance-verification data sheets report package input power and capacity, allowing buyers to calculate specific power from tested figures. The U.S. Department of Energy’s Improving Compressed Air System Performance guide also stresses that system pressure and operating conditions affect energy use. In practice, a 7.5 kW difference at a steady 10 m³/min changes the ratio by 0.75 kW per m³/min. That gap matters over long shifts. A tidy number can still mislead. Check whether the quoted flow is actual delivered capacity, not theoretical displacement, and review test tolerances. Then compare the result with your plant’s logged load: fixed-speed machines may unload during demand dips, using power while delivering little air. That detail is easy to miss.
In fixed speed screw compressors, motor efficiency deserves more attention than a simple horsepower comparison.
IEC 60034-30-1 classifies electric motors by efficiency classes, including IE3 and IE4. IE3 represents premium efficiency, while IE4 requires lower losses under defined test conditions. These ratings describe the motor, not the complete compressor package.
A reliable selection starts with the nameplate. Check rated power, voltage, frequency, duty, and efficiency at the intended operating point. A motor may achieve IE4 at its rated load, yet perform differently when the compressor runs lightly loaded. That detail is often missed.
Measure actual current, discharge pressure, running hours, and unloading frequency during a normal production shift.
Field data beats assumptions.
IE4 motors can reduce electrical losses, especially in plants operating continuously. They may also cost more and require careful attention to starting current, thermal limits, and replacement compatibility. Review the motor’s efficiency curve, not only its headline class. Ask for test documentation and declared operating conditions. Clear records improve purchasing decisions and future audits. Small errors matter.
For seven fixed speed screw compressor candidates, compare total energy use over several years. Include maintenance, cooling demand, installation limits, and expected load patterns.
An IE3 motor can sometimes be the practical choice when operating hours are low. IE4 is stronger when the compressor runs long shifts near full load.
The best answer is not always the highest rating.