For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615
Service & Repairs: 616-698-7500
24/7 Parts: 1-800-727-8780
sale@inlandmachineokc.com
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780

With a customized Stiles University course, we can provide expert training for your team, on-location. Whether it's programming, operation or maintenance, we want to help you train your personnel to meet your production goals efficiently and effectively.

Experience the trusted workforce development training and machinery knowledge you rely on from Stiles University, now at your convenience. With technology changing every day and new methods being developed constantly, Stiles University Online has the latest information and training content available at your fingertips.
616-698-7500

Do you want to produce more efficiently? Processes and flows are key. We optimize these together with you, re-organize them and make sure that you reduce your lead time and save costs. This enables you to implement customized manufacturing and achieve your business goals.

Industrialized construction is evolving. Automation, robotics and advanced technology are raising the level of productivity, efficiency and precision for builders in North America.

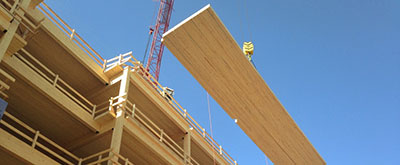
Stiles Machinery is at the forefront of providing technology and machining for producing high quality mass timber. Automated solutions for your mass timber production can increase your manufacturing quality and productivity.

Project management services from Stiles make it easy to streamline your entire project— from concept and consultation to integration and implementation.
For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780For support and service of your machinery, Stiles has experts available 24/7 to help reduce downtime and get you back in action.
Technical Support: 616-698-6615 Service & Repairs: 616-698-7500 24/7 Parts: 1-800-727-8780
Parts are available from Stiles 24 hours a day, seven days a week, and are shipped from our Grand Rapids, Michigan fulfillment center.
24/7 Parts: 800-727-8780For global buyers, choosing the right Carton Flow Racking Systems requires more than comparing prices and photographs. In 2026, warehouses face tighter delivery windows, mixed carton sizes, labor shortages, and frequent inventory changes. A reliable system must support fast picking without creating unsafe congestion.
John J. Bartholdi III, a respected warehouse operations researcher and Professor Emeritus at Georgia Tech, states, “The objective of order picking is to assemble the right items, in the right quantities, at the right time, in the right sequence, and at the lowest possible cost.” This principle remains highly relevant to Carton Flow Racking Systems. Gravity rollers, inclined lanes, and clear front access can shorten walking distances and improve stock rotation. Yet performance depends on real operating details. Carton weight matters. So does packaging friction.
Experienced buyers should examine lane depth, roller spacing, replenishment access, rack load capacity, and installation conditions. A system designed for small shoe boxes may perform poorly with irregular medical cartons or heavy beverage cases. Cold storage creates another challenge. Condensation may affect components and workplace safety.
No system is perfect. That matters.
This guide reviews the 2026 Best Carton Flow Racking Systems for Global Buyers through a practical and evidence-based lens. It considers picking speed, durability, maintenance, customization, worker ergonomics, and total ownership cost. It also recognizes an uncomfortable truth: the cheapest quotation can become the most expensive decision. Careful measurements, supplier verification, and pilot testing can reduce that risk. Still, every warehouse should reassess its assumptions before selecting a long-term storage solution.
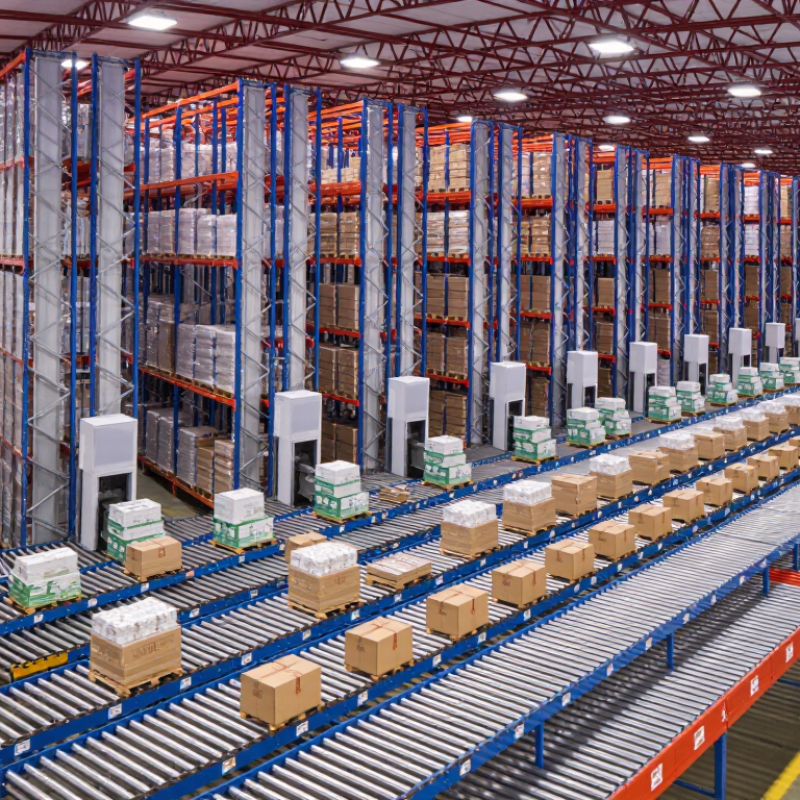
Carton flow racking is a gravity-fed storage system for cartons, totes, and small cases. Each lane contains slightly inclined rollers or wheels. Workers load products from the rear, while pickers retrieve them from the front. As one carton leaves, the next carton moves forward automatically. Simple, but not effortless.
The rack supports a clear first-in, first-out workflow. This helps warehouses rotate dated products and reduce hidden stock. Lane dividers keep cartons aligned, while brakes or speed controllers manage heavier loads. The slope must match carton weight, base material, and packaging quality. Too little slope can stop movement. Too much slope can cause impact damage.
In a working warehouse, a 1.2-meter lane may hold several cartons, depending on carton depth and clearance. Replenishment teams should inspect rollers, labels, and damaged packaging during each shift. A crushed carton can block an entire lane. That detail is easy to overlook. Carton flow also needs accurate slotting; fast-moving items belong near accessible pick faces, not in random spaces. Capacity calculations should include aisle width, product variation, and safe loading limits. A layout that looks efficient on paper may slow workers when cartons differ in size. Testing one live section before full installation is a sensible, though sometimes neglected, step.
Carton flow racking uses inclined roller or wheel tracks to move cartons from the replenishment side to the picking side by gravity. The chart shows the estimated number of 150 mm-deep cartons that can fit in one lane at common lane depths. Actual capacity varies with carton size, clearance, roller design, and rack configuration.
2026 Best Carton Flow Racking Systems for Global Buyers
Key Design Features of Modern Carton Flow Racking Systems
Modern carton flow racking systems use inclined roller tracks to move cartons toward the picking face. Gravity does the routine work. This design supports first-in, first-out rotation and reduces unnecessary walking in busy warehouses. Adjustable lane widths help operators handle different carton sizes. However, poorly matched widths can cause cartons to tilt, stall, or collide.
Strong frames, reliable wheel assemblies, and reinforced guides support daily warehouse use. Each lane should match the carton weight, base shape, and replenishment method. Adjustable dividers improve product separation and reduce picking errors. Clear labels also matter, especially when several languages or product codes appear in one facility. Safety stops and rear guides help prevent cartons from falling during loading.
Tips: Test sample cartons before ordering. Check movement at low and high loads. Inspect rollers, brakes, and fasteners regularly. Leave enough aisle space for safe replenishment. Corrosion-resistant finishes may suit humid storage areas. Do not assume one pitch works for every carton. A practical trial often reveals problems that drawings miss. Perfect planning is rare. Careful measurement and honest review create a safer, more dependable system.
Key Design Features of Modern Carton Flow Racking Systems
| Design Dimension | Typical Specification | Recommended Configuration | Operational Benefit | Buyer Considerations |
|---|---|---|---|---|
| Carton Load Capacity | Approximately 5–80 kg per carton, depending on the roller track and lane width | Use light-duty tracks for small parcels and reinforced tracks for heavy cases | Supports gravity movement without powered conveyors in many picking applications | Confirm the maximum carton weight, bottom stiffness, and load distribution before selection |
| Roller Track Type | Plastic wheels, steel rollers, or skate-wheel tracks | Plastic wheels for lightweight cartons; steel rollers for higher loads and frequent replenishment | Provides controlled carton flow and adapts the rack to different packaging conditions | Evaluate noise, rolling resistance, corrosion exposure, and maintenance access |
| Track Incline | Commonly about 3°–8°, subject to carton size, weight, and track design | Use a lower incline for fragile or unstable cartons and a higher incline for reliable movement of heavier cartons | Creates gravity-fed FIFO movement from the replenishment side to the picking side | Test representative cartons because excessive slope can increase impact and product damage |
| Lane Width | Typically 300–1,200 mm, with custom widths available for mixed carton sizes | Select a lane slightly wider than the carton width to allow smooth loading and unloading | Improves product accessibility while reducing carton jams | Base the width on actual carton dimensions, tolerances, labels, and packaging deformation |
| Lane Depth | Commonly 1,200–3,600 mm; deeper lanes hold more cartons but require tighter flow control | Use short lanes for high-SKU, high-turnover products and deeper lanes for stable fast-moving SKUs | Balances storage density with replenishment frequency and inventory visibility | Check SKU velocity, replenishment cycles, carton quantity per lane, and available rack depth |
| Carton Size Range | Often designed for cartons from approximately 150 × 100 mm to 800 × 600 mm | Use adjustable dividers and modular tracks for mixed-size carton storage | Allows one rack structure to handle multiple product categories | Verify the smallest and largest carton footprints, heights, and center-of-gravity conditions |
| FIFO Control | Front access with rear replenishment and lane-level stock rotation | Install rear loading access, lane labels, and positive carton stop controls | Helps reduce product aging and supports date-sensitive inventory management | FIFO performance depends on correct loading discipline and unobstructed track movement |
| Carton Separators | Adjustable steel or polymer dividers positioned along each lane | Choose tool-free adjustable dividers for frequently changing SKU assortments | Prevents cartons from shifting between lanes and improves item identification | Confirm divider height, spacing adjustment, edge protection, and compatibility with cartons |
| Entry and Exit Stops | Front carton stops, rear retaining rails, and optional brake rollers | Use brake rollers or speed controllers for heavy cartons and long lanes | Controls carton speed and reduces impact at the picking face | Select stop components according to carton mass, slope, and operator ergonomics |
| Rack Frame Height | Common installations range from approximately 1,800 mm to 6,000 mm | Match beam levels to carton height, picking ergonomics, and replenishment equipment | Uses vertical warehouse space while maintaining practical access | Consider ceiling height, sprinkler clearance, seismic requirements, and lifting equipment |
| Load per Rack Level | Frequently engineered within approximately 300–1,500 kg per level | Specify level capacity based on the maximum number and weight of cartons stored | Supports stable storage and reduces the risk of beam or frame overload | Require structural calculations for the actual layout, loading pattern, and local regulations |
| Material and Finish | Cold-formed or structural steel with powder-coated or galvanized components | Use powder coating for dry indoor warehouses and galvanized finishes for humid or corrosive areas | Improves durability, visibility, and resistance to routine warehouse wear | Review coating thickness, corrosion exposure, cleaning methods, and local fire requirements |
| Picking Ergonomics | Frequently picked cartons positioned between waist and shoulder height | Combine flow lanes with ergonomic working heights, clear labels, and accessible replenishment zones | Reduces bending, reaching, and unnecessary walking during order picking | Assess worker height range, carton weight, picking frequency, and manual handling limits |
| Modularity and Expansion | Bolt-in tracks, adjustable beams, movable dividers, and expandable rack bays | Choose modular components when SKU profiles or throughput are expected to change | Simplifies reconfiguration and reduces the need for complete rack replacement | Confirm spare-part availability, future bay compatibility, and installation requirements |
| Safety Features | Back guards, end protectors, aisle guards, anti-collapse features, and load notices | Add protection where forklifts, pallet trucks, or powered handling equipment operate nearby | Helps protect operators, cartons, rack frames, and adjacent warehouse equipment | Apply local rack safety standards and schedule routine inspections after installation |
| Best-Fit Applications | E-commerce fulfillment, spare parts, retail distribution, food packaging, and light manufacturing | Use carton flow for high-SKU operations requiring frequent manual picking and replenishment | Improves pick density, stock rotation, and order preparation speed | For pallets, very irregular loads, or low-velocity inventory, consider other storage systems |
Planning note: Dimensions and capacities shown are typical engineering ranges for modern carton flow installations. Final specifications should be confirmed through site measurements, carton testing, structural calculations, and applicable local safety requirements.
Selecting a carton flow system starts with warehouse work, not a catalog. Measure carton length, width, height, weight, and daily order volume. Record the smallest and largest cartons separately. A narrow product range may suit fixed roller lanes. Mixed cartons need adjustable dividers and adaptable lane widths. Fast-moving items require smooth replenishment and clear picking access.
Match the rack design to your operating method. FIFO lanes support date-sensitive stock and regular rotation. Gravity rollers can reduce reaching, but their pitch must fit carton bases. Lightweight cartons may stop on unsuitable rollers. Heavier cartons need stronger frames, brakes, and lane controls. Check aisle width, shelf height, replenishment equipment, and worker reach before approving the layout. Small details matter.
A pilot lane is often more reliable than a perfect-looking drawing. Test real cartons during busy picking periods. Watch for jams, label visibility, awkward bending, and replenishment delays. The choice is rarely perfect on the first attempt. One practical mistake is sizing lanes from carton dimensions alone. Product overhang, damaged packaging, and seasonal volume can change performance. Require load data, installation guidance, inspection records, and compliance with local warehouse safety requirements. This evidence helps global buyers compare suppliers without relying on attractive claims.
For global buyers, carton flow racking should be judged beyond price. In warehouse reviews, I check frame stability, roller alignment, wheel durability, and load labels. A rack may look robust yet perform poorly when cartons vary in size. Ask for steel grades, coating details, load calculations, and test records. Clear drawings matter. They reduce installation errors across languages and time zones.
Compliance requirements differ by destination, building design, and fire-safety planning. Request current inspection documents and confirm whether local engineers must approve the layout. Do not treat a familiar certificate as universal proof. It may not be accepted. Shipping also needs attention. Confirm packed dimensions, gross weight, pallet count, and moisture protection before booking freight. Verify Incoterms, customs paperwork, spare parts, and damage-report procedures. A bent guide rail can delay commissioning more than expected.
Tips: Compare at least three technical quotations using the same load assumptions. Request a sample roller or joint photo. Check carton dimensions from real orders, not ideal samples. Keep a written acceptance checklist. It sounds basic. It prevents arguments. Leave room for human error; measurements can be wrong, and suppliers may misunderstand a drawing. Recheck critical dimensions before production.
Carton flow racking performs best when installation matches the carton size, load weight, and picking rhythm. Before assembly, confirm floor levelness, aisle clearance, beam capacity, and local safety requirements. Use calibrated tools to check frame alignment. Even a small tilt can make cartons drift unevenly.
Experienced installers secure each frame, roller track, guide rail, and end stop before loading inventory. Test every lane with empty cartons first. Then use representative cartons at different weights. I have seen teams overlook soft packaging, causing cartons to stall halfway. That mistake reduces both speed and operator confidence. Load labels should remain visible and readable.
Maintenance needs a simple, documented routine. Inspect rollers, axles, supports, and stop plates weekly in busy zones. Remove dust, tape, and broken packaging immediately. Replace damaged components instead of bending them back. Record jams by lane, product type, and shift. These details reveal recurring problems. Performance improves when replenishment follows a fixed direction and pickers avoid mixing carton sizes randomly. Measure travel time, blocked lanes, replenishment errors, and damaged cartons each month. Review the data with warehouse staff, because the original layout may not fit real working habits. Small adjustments often help, but some layouts need deeper redesign.